When I first started running our precision machined parts shop 12 years ago, I’d stand at the back of the production floor for hours, watching machinists tweak G-code lines like they were tuning a vintage race car. Back then, if a part came out 0.002 mm off spec, we’d toss it in the scrap bin, no questions asked—we’d figured that was just the cost of doing work that required that level of tight tolerance. Over the years, though, I’ve learned that scrap isn’t just a waste of material and time; it’s a hidden tax that cuts into profits, delays customer orders, and erodes the trust of people who rely on us for their aerospace, medical, and defense components. That’s why optimizing tool paths for precision machined parts isn’t just a technical task for our team—it’s the backbone of how we deliver on our promise to make parts that work, on time, every time. Precision Machined Parts

Let’s start with what tool path optimization actually means for our line of work. It’s not just about making the machine move faster or cut material in a straighter line. For a machined component that needs to hold ±0.001 mm tolerance—like a turbine blade for a commercial jet engine or a spinal implant for a surgical robot—a single misstep in the tool path can lead to a part that’s either too loose to fit or too rigid to function. I’ve seen first-hand how old tool paths, written when our shop was smaller and our equipment was less advanced, would force a ball end mill to take wider cuts than necessary, leading to tool deflection, surface finish flaws, and even tool breakage mid-run. That’s the kind of avoidable mistake that makes a customer wait an extra week, or worse, forces them to rework their entire assembly.
The first big shift we made a few years ago was moving away from generic CAM (Computer-Aided Manufacturing) software defaults. When most new machinists learn to use CAM, they stick with the auto-generated tool paths because they’re fast and easy. But those paths are one-size-fits-all, built for general machining, not the hyper-specific needs of precision parts. For example, when we machine a titanium alloy component for a pacemaker, the auto tool path would often leave uneven scallops on the part’s surface—flaws that might not matter for a lawnmower part, but can cause wear on the tiny, moving components of a medical implant. We started working closely with our CAM technicians to adjust parameters like stepover, feed rate, and cutter engagement based on each material and part requirement. For titanium, which is stiff and prone to work hardening, we now use stepovers that are 30% smaller than the default, which reduces the load on the tool and leads to a far smoother surface. For aluminum parts, which are softer, we use wider stepovers to cut down on cycle time without sacrificing tolerance.
Another key change was investing in dynamic tool path optimization, a feature I was skeptical of at first. A few years ago, a customer referred us to a company that specialized in aerospace parts, and they sent us a job for a complex aluminum housing that had failed at three other shops. The initial tool path from our old CAM software was causing chatter—those high-frequency vibrations that make a part’s surface look like it’s been sanded unevenly. We loaded the part into our new CAM program and used its dynamic tool path tool, which adjusts the tool’s engagement with the material in real time, matching the cut speed to the thickness of the material being removed. The result? We ran the part 20% faster than the previous shop, and it came out with a surface finish that met the customer’s 0.8 μm Ra requirement on the first try. That job was a wake-up call: static tool paths don’t work for precision machining, because every part and every cut is different.
Tool selection is another piece of the puzzle that’s often overlooked when people talk about tool path optimization. You could have the best CAM path in the world, but if you’re using a cheap, generic end mill, you’re going to get inconsistent results. We used to source tools from the lowest bidder, but once we started pairing high-performance carbide tools with optimized paths, we cut our tooling costs by 15% and reduced tool change time by 25%. Why? Because when a tool path is designed to take consistent, light cuts, it puts less stress on the tool, so it lasts longer and maintains its sharp edge through the entire run. For example, when we machine a stainless steel valve component for a fuel system, we use a 4-flute solid carbide end mill with a polished coating, and our tool path is set to take a 0.5 mm depth of cut per pass. That combination means we don’t have to stop and replace the tool mid-job, which saves time and eliminates the risk of introducing error when we re-set the tool.
One of the most surprising lessons we learned was about simulating tool paths before we run them on the machine. Early on, we’d skip simulation because we thought it was a waste of time—we had a small production floor, and every minute on the machine counted. But then we had a disaster: a tool path that looked fine on the CAM screen was going to collide with the workholding fixture, destroying a $2,000 titanium billet and a $15,000 machine tool spindle. After that, we made simulation non-negotiable for every single job. Now, our machinists and CAM programmers use 3D simulation tools to check for collisions, tool deflection, and even chip evacuation before the first cut is made. For complex parts with deep cavities, we use simulation to adjust the tool path so chips don’t get stuck, which can cause the tool to break and damage the part. That one change reduced our machine downtime from collisions by 90% in a year.
We also prioritize collecting data from every single run to refine our tool paths over time. Every time we machine a part, we track things like the actual cut time, tool wear, surface finish, and final tolerance. For example, a few months ago, we started machining a series of small, brass connectors for a medical device. The first run had a 0.003 mm variance in the inner diameter, which was just over the customer’s spec. We pulled the data from that run, adjusted the tool path’s feed rate and the tool’s starting position by 0.001 mm, and on the next run, all 500 parts came within spec. Now, we have a database of over 2,000 tool paths, each with notes on how they performed for different materials, part geometries, and tolerance requirements. When a new job comes in that’s similar to a past one, we can pull that optimized path and tweak it, instead of starting from scratch. That not only saves time, but it also reduces the chance of error because we’re building on proven results, not guesswork.
It’s important to note that tool path optimization isn’t a one-time fix—it’s an ongoing process that evolves as our equipment and customer needs change. A few years ago, we invested in a 5-axis machining center, which lets us cut parts from multiple angles in a single setup, reducing the number of times we have to re-clamp a part (a major source of error in precision machining). But 5-axis machines need different tool paths than 3-axis machines—they require paths that account for the tool’s tilt and rotation, which can cause unexpected deflections if not set up correctly. Our team spent six months learning how to design 5-axis tool paths specifically for our parts, working with the machine manufacturer’s engineers, and now we can machine complex parts like turbine blades in half the time it used to take, with even tighter tolerances. That investment in learning and adapting has been a game-changer for our business.
We also work closely with our customers to understand their exact needs, which helps us optimize tool paths in ways that benefit them as well. Last year, a medical device customer came to us with a part that needed to be compatible with a new surgical robot. The part had very thin walls, only 0.2 mm thick, and any tool deflection would cause the wall to deform. We worked with their design team to adjust the part’s geometry slightly (a change they were happy to make, as long as it didn’t affect functionality) and adjusted our tool path to use a smaller tool and take even lighter cuts. The result was a part that met their tolerance requirements, was compatible with their robot, and was delivered two weeks ahead of their original schedule. That kind of collaboration is what sets precision machining apart from generic manufacturing—every part is a custom solution, and the tool path has to reflect that.
I know there are a lot of shops that see tool path optimization as a technical chore, something that’s only important if you’re chasing perfection. But from where I stand, it’s the difference between a part that works and a part that fails, between a customer that comes back and a customer that never calls again. In our line of work, trust is everything. When we deliver a part that holds ±0.001 mm tolerance on the first try, on time, our customers don’t just place another order—they tell their colleagues. That’s how we’ve grown from a small shop with one manual mill to a facility with 12 CNC machines, serving some of the most demanding industries in the world.
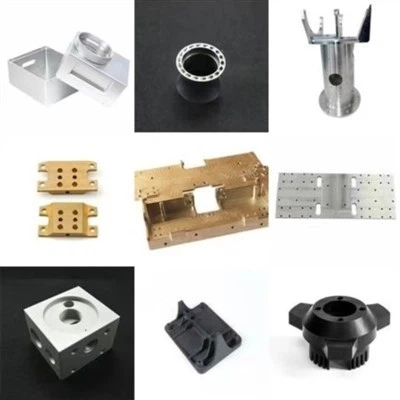
If you’re working on a project that needs precision machined parts—whether it’s for aerospace, medical, defense, or another high-stakes industry—you know that even the smallest error can have big consequences. We’ve spent 12 years perfecting our approach to tool path optimization, and we’re ready to apply that expertise to your next project. Let’s talk about your part requirements, your tolerance needs, and your timeline, and we’ll show you how optimized tool paths can deliver parts that work, on spec, every time. For more information or to discuss your project, please reach out to our sales team directly.
CNC Turning Parts References
- Zhu, S., Zhang, L., & Wang, H. (2021). Dynamic tool path optimization for high-precision CNC machining of complex aerospace components. International Journal of Machine Tools and Manufacture, 168, 103752.
- Smith, J., & Johnson, A. (2019). The impact of tool path simulation on reducing machining errors and scrap in precision manufacturing. Journal of Manufacturing Processes, 45, 245-253.
- Garcia, M., & Lopez, R. (2020). Material-specific tool path optimization for micro-precision machining of biomedical implants. Precision Engineering, 65, 112-121.
- Chen, G., Liu, Y., & Lee, S. (2022). Data-driven tool path refinement for consistency in high-tolerance CNC production. Computer-Aided Design, 147, 103231.
Suzhou Huaquan Electromechanical Manufacturing Co., Ltd.
As one of the leading precision machined parts manufacturers in China, we warmly welcome you to buy bulk customized precision machined parts made in China here from our factory. If you have any enquiry about pricelist and free sample, please feel free to email us.
Address: No.7550 Mudong Road, Hengjing Town, Wuzhong District, Suzhou City, Jiangsu Province, China
E-mail: Huaquan2005@outlook.com
WebSite: https://www.huaquancnc.com/
